How to Choose Food Grade Laminating Adhesive for Packaging
Choosing Food Grade Laminating Adhesive is not just a matter of picking a product labeled for food packaging. The adhesive must suit the exact film, foil, or paper layers in the package. It also needs to perform through lamination, curing, filling, transport, and storage. Yet no single formulation fits every structure. That matters. A pouch for dry snacks faces different demands from a pack holding oily or moist food.
Start with the package itself. Note each substrate, coating, print layer, and intended use. Then compare adhesive options for bond strength, clarity, odor, cure time, and resistance to heat or contents. Small details count. A sample may look smooth after lamination but still need adequate curing before conversion or filling. Ask suppliers for current technical and food-contact documentation that applies to your specific materials and intended market. Independent testing may also be appropriate; product names alone cannot confirm suitability.
Production conditions matter, too. Line speed, coating weight, temperature, and humidity can change results. Teams sometimes focus on initial tack and overlook how a bond behaves after aging. I have found that a simple trial plan helps: record settings, inspect finished samples, and test them under realistic storage conditions. It takes time. If results vary, pause and investigate rather than assuming the adhesive is at fault. Careful selection combines documented specifications with practical validation, while recognizing that each packaging design has its own limits.
What Food-Grade Laminating Adhesive Is and How It Works
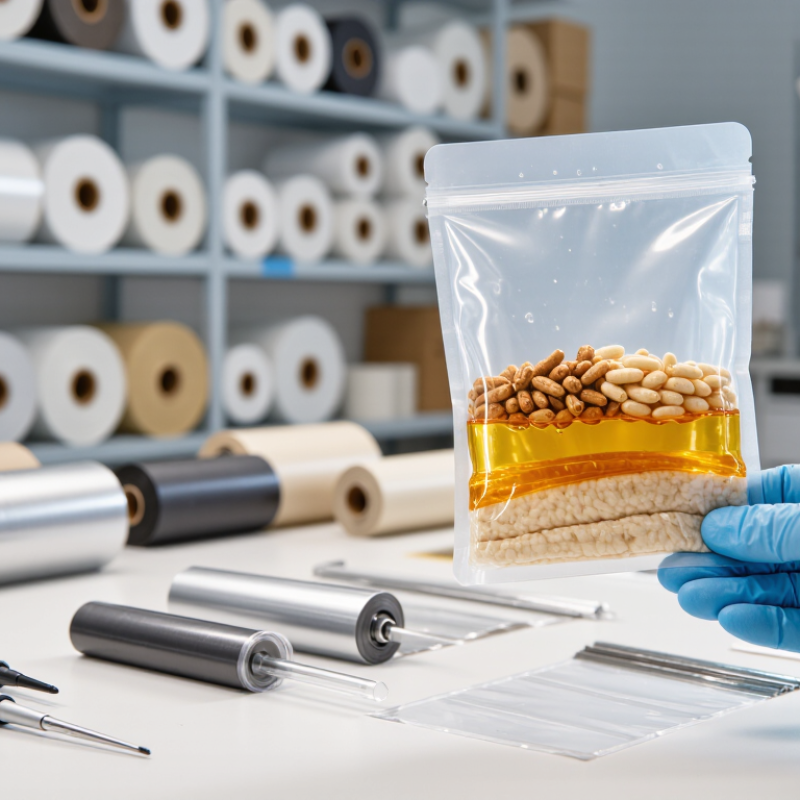
Food-grade laminating adhesive bonds layers such as printed film, aluminum foil, and paper into one flexible structure. It is applied as a thin coating, then pressed against another web. Depending on its chemistry, the adhesive may dry as water or solvent leaves, or cure through a reaction between components. The result is a laminate that can resist peeling and help protect food from moisture, oxygen, or odors.
The adhesive sits inside the package, but that does not make the whole package automatically suitable for food contact. Intended food type, storage temperature, contact time, and packaging structure all matter. During production, coating weight and curing conditions need careful control; incomplete cure can affect odor, bond strength, or migration performance. Details matter. Ask for technical data and food-contact documentation for the intended use, then verify the finished structure with appropriate testing. A fast bond can look convincing on the line, yet still need time to develop fully. That is easy to overlook. Test real samples, not just a neat laboratory strip.
Which Food-Contact Requirements Apply to Your Packaging
Which Food-Contact Requirements Apply to Your Packaging
Food-contact requirements depend on the markets where your package will be sold and how it will be used. A pouch holding oily snacks at room temperature presents different conditions from a pack designed for hot filling. Check the applicable rules for the food type, contact time, temperature, and intended use. Requirements can vary by region, so avoid assuming one document covers every market.
In a laminated structure, adhesive may sit behind a film rather than touch food directly. Still, migration can matter, especially with thin layers, high temperatures, or long storage. Ask suppliers for composition and compliance documents for the specific adhesive and intended packaging conditions. Review whether testing reflects your real structure, not just a similar sample. A checklist helps, but it can miss details; honestly, packaging teams sometimes discover those gaps late.
Tips: Record food type, filling temperature, and shelf life before choosing an adhesive. Keep test reports and supplier declarations together. If conditions change, reassess the evidence.
How to Assess Packaging Materials and Lamination Conditions
Assess the complete package, not just the film names. A PET-to-PE laminate behaves differently from foil-based structures under heat, pressure, and moisture. Check each layer’s thickness, surface treatment, and supplier specifications. Smithers’ report, The Future of Flexible Packaging to 2028, estimates the global market reached about US$271.7 billion in 2023. That scale makes material compatibility a practical concern, not a minor detail. Confirm the adhesive suits the food-contact application and the converting line’s speed and temperature.
Then map the actual lamination conditions. Record nip pressure, web tension, coating weight, drying temperature, and residual solvent risk. Ask whether the line uses solvent-based, solvent-free, or water-based adhesive; each needs different process controls. Test bond strength after the stated cure time, and repeat tests after aging or exposure to heat and moisture. A smooth film can still delaminate. Lab results may not match a fast production run, so validate on the real line.
Tips: Keep a small sample from each trial. Note settings and cure time. Check for haze, odor, bubbles, and edge lift. ASTM F88 can help assess seal strength, but it does not replace a full laminate evaluation. Small details matter. One overlooked setting can weaken the bond.
How to Compare Adhesive Types for Safety and Performance
“Food grade” is not a single adhesive formula. It means suitability for specific food-contact conditions. For dry foods, water-based adhesives may help limit solvent-related concerns. Solventless polyurethane systems can deliver strong bonds, but depend on accurate mixing and adequate curing. Solvent-based systems may suit certain film combinations, yet require careful residual-solvent control. Small details matter.
Compare options against the food type, packaging layers, storage temperature, shelf life, and production speed. Request relevant compliance documents and migration or extractables data for the intended structure and use. A technical data sheet is a useful start, not proof for every package. During a production trial, check bond strength after aging, odor, seal integrity, and film curl—not only the initial peel result.
The Flexible Packaging Association’s 2024 State of the Industry report put U.S. flexible-packaging sales at $42.9 billion in 2023. That scale makes consistent performance important. But scale is not a safety metric.
It is easy to overvalue a strong initial bond; that assumption deserves a second look.
How to Verify Adhesive Compliance Before Production
Before production, verify the adhesive against the packaging’s intended food, contact conditions, and sales markets. Request a current declaration of compliance, technical data sheet, safety data sheet, and supporting test reports. Check that documents identify the exact adhesive formulation and laminate structure, not just a product family. Conditions matter: hot filling, long storage, fatty foods, and direct contact can change migration risks. Ask whether testing covered the finished laminate under conditions matching your use.
The Flexible Packaging Association’s 2024 State of the U.S. Flexible Packaging Industry report estimates 2023 sales at $42.9 billion, about 21% of the U.S. packaging market. That scale makes traceable verification practical, not optional. Review migration data, residual-solvent results where relevant, cure time, and the test laboratory’s methods. Keep the adhesive batch number, production settings, and retained laminate samples together. Small details count. A certificate can look complete and still omit the intended food type or temperature. I would pause production if those conditions are unclear, even when the paperwork feels familiar.
How to Choose Food Grade Laminating Adhesive for Packaging
Verify the adhesive and finished laminate against the regulations and intended conditions of use for the target market.
Before production: Review supplier declarations and composition information, then confirm migration testing on the finished packaging under conditions representative of its intended use. The EU limit shown is for applicable plastic food-contact materials; it is not a universal adhesive-specific limit. Requirements vary by material, market, food type, and use conditions.